time:2026-11-13 13:33:45Views:
Drives, operator panels and automation components were exported to Vietnam as a MINGCHENG automation control package. Getting these parts to work together is an integration job, not just a purchasing job.
Drives, operator panels and automation components were exported to Vietnam as a MINGCHENG automation control package. Mixed components only behave like a system once the communication scheme is agreed.
That is why the motor list, the HMI screens and the fieldbus layout belong in the same specification.
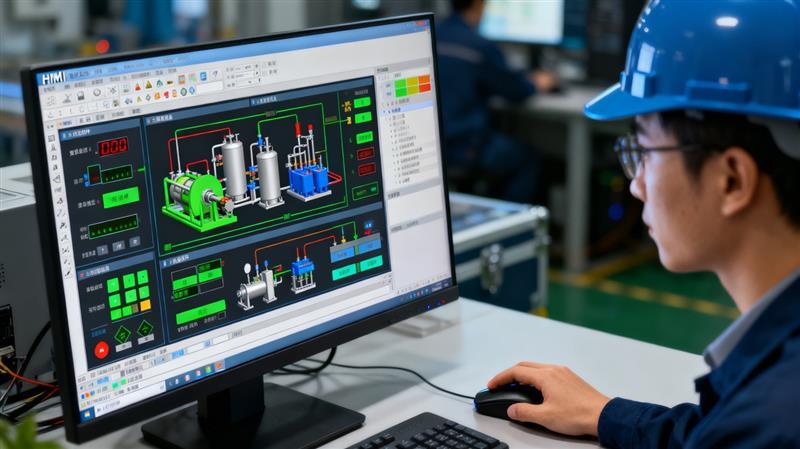
A typical package combines drives for motor speed control, an HMI for operator input and status display, a PLC or controller for sequencing, and the field devices that report back. Each item can be specified correctly on its own and still cause problems if the communication interfaces do not line up.
Deciding on one fieldbus or one clear analogue scheme before ordering saves the most commissioning time. Mixed protocols are solvable, but they add gateways and another point of failure.
An industrial automation control system for Vietnam should be specified around one agreed communication scheme, otherwise HMI and VFD integration becomes a gateway project.
An operator panel should show the values people actually use: running frequency, motor current, fault history and a simple way to acknowledge alarms. Overloaded screens slow down fault diagnosis, especially on a night shift with a small crew.
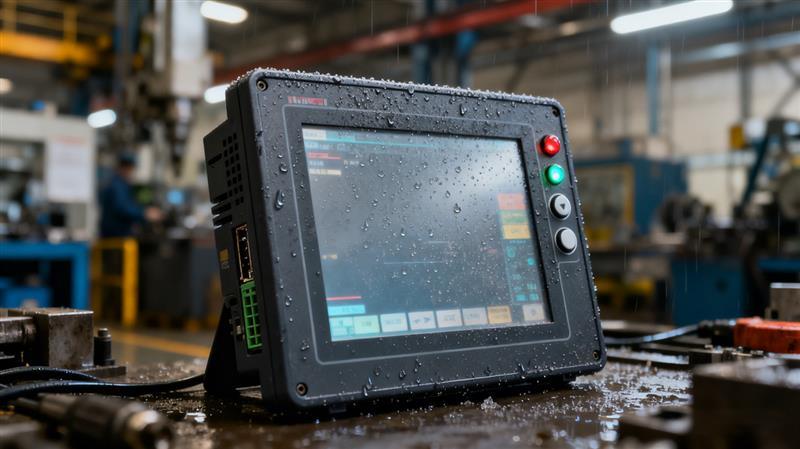
Panel enclosure rating, screen visibility under workshop lighting, and language support are worth confirming at the specification stage. They are cheap to define and awkward to change after the cabinet is built.
HMI panel configuration is where the operator experience is decided: running frequency, motor current, fault history and a simple alarm acknowledge belong on the first screen.
Most early problems are signal wiring and grounding rather than device faults: a shielded cable grounded at both ends, an analogue signal routed next to a motor cable, or a missing termination resistor on a fieldbus segment.
A simple point-to-point signal check before the first production run catches nearly all of these, and a documented parameter backup makes later troubleshooting much faster.
As an industrial automation control system supplier China, MINGCHENG ships the parameter backup with the MINGCHENG automation control package rather than leaving it to be recreated on site.
Components are powered and checked as a set before dispatch, with the communication option and the agreed panel configuration verified. Manuals, the parameter backup and a small set of consumable spares are packed with the shipment.
Confirming the motor list and the control philosophy up front allows the drive parameters and screen layout to be prepared in advance, which shortens the work on site.
A fieldbus commissioning checklist covering shielding, termination and cable routing catches most faults before the first production run.
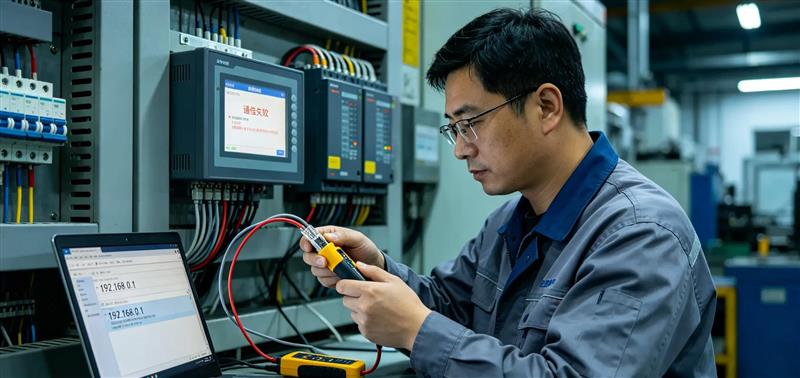
Fix the fieldbus or analogue scheme before ordering components, and ask for the motor list and control philosophy to be used to prepare parameters and screens in advance. Mixed protocols are solvable, but they add a gateway and another point of failure.
Keep a documented parameter backup and a fieldbus commissioning checklist with the cabinet. Both are cheap to produce at dispatch and are the first things a maintenance team needs after a device swap.
Drives for motor control, an HMI for operator interaction, a controller for sequencing, and the field devices that provide feedback, all on an agreed communication scheme.
They need gateways and extra configuration, which adds commissioning work and another component that can fail.
Shielding and grounding mistakes, analogue signals routed beside power cables, and missing fieldbus termination rather than defective devices.
Agree one fieldbus or analogue scheme, list every motor and its nameplate data, define the screens operators need, and request a fieldbus commissioning checklist and a parameter backup with the shipment.
Share your motor list and preferred control interface with MINGCHENG, and we will put together a matched drive, HMI and control package.
Keep up on our always evolving product features and technology. Enter your e-mail and subscribe to our newsletter.